Global supply chains are once again under pressure, with the conflict in the Middle East pushing up the cost of base oils, additives and transportation. For manufacturers, machine shops and maintenance teams, this means one thing: metalworking fluids and lubricants are about to significantly increase, and in some cases be harder to source. If you run CNC machines, lathes, mills or grinding operations, now is the time to tighten control of your coolant systems. Optimising your fluid management won’t just save money, it will reduce downtime, improve tool life, enhance operator safety, and keep production running smoothly during unpredictable times. In this article, we’ll explore three high-impact, practical strategies to help you extract every bit of value from your coolant: 1: Get concentration under control 2: Keep coolant clean and contamination-free 3: Recovery of fluid from swarf These insights are based on shop floor observations from Bob Dulieu, one of our Technical Sales Managers who visit UK machine shops every week.
1. Coolant Concentration: Why it Matters More Than Ever
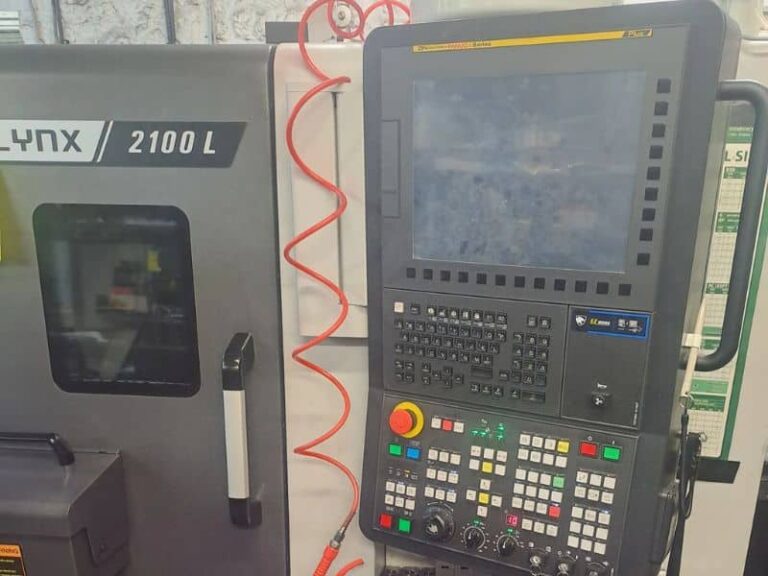
One of the biggest and most expensive mistakes we see in machine shops is incorrect coolant concentration. And with prices rising, hidden waste is becoming painful. Recently our team inspected a hardworking Doosan CNC running a coolant designed for a 4–10% concentration range with a refractometer conversion factor of 1.33. The machine tested at 14% Brix, which multiplied by the refractometer conversion factor equals a true concentration of 18.6%, nearly double the recommended upper limit.
Why this matters:
- The sump held around 150 L
- At the correct concentration, it only needed 10–14 L of concentrate
- Instead, it contained 28 L
- That’s 18 L of unnecessary concentrate
- At around £5.00 per litre, that’s £90 in wasted product in one machine
- Multiply across ten machines and you’re burning £900+ unnecessarily
And the cost isn’t just financial. Over-concentrated coolant can also contribute to foaming and skin sensitisation. Getting concentration right is one of the simplest and most effective ways to reduce coolant waste and improve performance. When levels drift too high or too low, costs rise, machines misbehave and operators often feel the effects first. A few consistent habits can keep your coolant exactly where it should be, protecting your budget, your operators and your equipment.
How to fix it Coolant Concentration:
- Check concentration routinely
- Know your coolant’s Brix reading and conversion factor
- Record actual vs target ranges
- Automate the mixing process by using a Mixtron Dosing Pump
- Standardise fluid top-ups
- Use digital tools like PROCARE Fluid Cloud to log, track and analyse results
Small improvements here generate big savings, especially when coolant prices spike.
2. Keep Coolant Clean: Control Tramp Oil & Swarf Build-Up
If concentration is the first pillar of coolant performance, cleanliness is the second. The majority of coolant failures we diagnose link back to tramp oil, swarf accumulation and bacterial activity.
Tramp oil causes multiple problems:
- Feeds bacteria
- Creates anaerobic zones where microbes thrive
- Emulsifies, reducing lubrication
- Increases tool wear (a major concern with carbide prices soaring)
- Causes smoking and misting issues
- Increases risk of operator dermatitis
Swarf build-up leads to:
- Pump starvation and foaming
- Delayed coolant return
- Metallic contamination leaching into the fluid
- Blocked filters and disrupted flow
- Displaced coolant volume causing heating and bacterial growth
So, How can you prevent it?
- Skim tramp oil regularly
- Remove swarf frequently, don’t let it sit in the sump
- Use surface skimmers or a Freddy vacuum
- Keep sumps as clean as possible between service intervals
- Test and monitor bacteria, pH and concentration
- Maintain accurate records and act when parameters drift
Good housekeeping adds months to fluid life, which is a huge win during volatile supply periods.
3. Maximise Coolant Recovery from Swarf
Swarf drag-out is unavoidable, but losing coolant into the swarf bin doesn’t have to be. Historically, shops would let swarf bins fill with fluid, then tip the entire mix, coolant, metal fines and all back into the sump or down the drain. Today, with rising prices and growing environmental pressure, coolant recovery is one of the easiest ROI wins in the machine shop.
Modern recovery solutions:
- Freddy vacuums: filter coolant from sumps and return clean fluid
- Coolant recycling systems: recondition spent coolant from swarf briquetting
- In-bin recovery systems like CoolReturn: pulse clean fluid back into the sump continuously
The benefits:
- Reduce coolant purchasing
- Extend fluid life
- Lower disposal costs
- Protect environmental compliance
- Improve machine performance
- Reduce downtime
The maths behind coolant recovery has never been more compelling, particularly as prices rise. Just remember: recycling only works if the coolant is in good condition to start with. Regular testing, good housekeeping and clean swarf bins are essential. Coolant recovery can make sense in the right environment, it would be worth speaking to your metalworking fluid provider for advice on finding the right solution for your workshop.
Final Thoughts: Optimise Now to Protect Your Operation Later
Times are challenging, but challenges create opportunities. With metalworking fluids rising in cost and complexity, there has never been a better moment to:
- Control coolant concentration
- Keep systems clean
- Recover as much fluid as possible
- Track and record everything properly
- Use digital tools to automate and improve consistency
A well-maintained coolant system lasts longer, performs better and saves money. If you want support with coolant testing, automated dosing, operator training, or implementing a complete coolant management programme, our team and our PROCARE Fluid Management service is here to help. Get in touch to find out how our team can help, our advice is always FREE! Call 0114 285 2987 or email [email protected]